

Malaysia Kitchen Equipment Maker Buys 304 No.4 HL and BA Stainless Steel Sheet 1.5mm 1.8mm 2mm
Published On: November 13, 2026
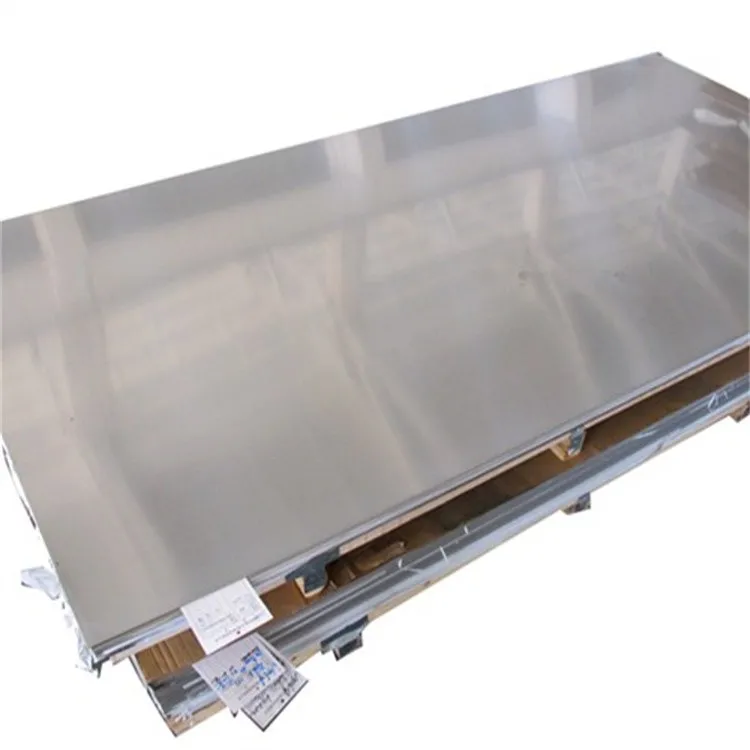
A stainless steel fabricator in Selangor, Malaysia has consolidated its flat-product purchasing with a single mill for 304 No.4 HL finish stainless steel plate and 304 BA finish stainless steel sheet in 1.5mm, 1.8mm and 2.0mm gauges. The three thicknesses now cover the company's full commercial kitchen range, removing the mixed-mill inconsistencies that had driven rework on every batch.
The buyer is a mid-sized fabricator supplying stainless steel commercial kitchens, food processing benches and laundry equipment to hotel groups, chain restaurants and institutional projects across Peninsular Malaysia and Singapore. Its workshop runs laser cutting, CNC bending, TIG welding and a polishing line. Annual consumption of 304 sheet sits in the range of 300 to 400 tonnes, split mainly between hairline and bright annealed surfaces.
- Mixed sources, mixed appearance. Sheet bought from three different traders produced visible shade and grain mismatch when panels from different coils were welded side by side on the same cabinet run.
- Thickness drift on the light gauges. Nominal 1.5mm material arriving between 1.32mm and 1.48mm forced the bending team to re-set tooling per bundle and caused springback variation.
- Surface damage in transit. Without proper interleaving and film protection, No.4 HL panels arrived with scuff marks that had to be re-polished, adding labour hours per project.
- Long and unpredictable replenishment. Import lead times of six to eight weeks made it difficult to promise installation dates to hotel clients with fixed opening schedules.
- Documentation gaps. Specifiers increasingly asked for mill certificates traceable to heat number and compliant with ASTM A240.
We proposed a single-source supply programme covering both finishes in the three requested gauges, drawn from one steel mill and one polishing line so that grain direction, gloss level and colour tone stay consistent across every coil in the programme. No.4 HL finish is produced by a controlled abrasive belt sequence that lays a continuous hairline grain with a Ra of 0.4 to 0.8 micron, giving the brushed look that dominates commercial kitchen fronts and elevator interiors. BA finish is achieved by bright annealing in a controlled atmosphere followed by skin pass, producing a mirror-bright, chromium-rich surface with no mechanical polishing step, preferred for splashbacks and display liners that must resist staining.
Thickness is held to plus or minus 0.05mm on 1.5mm and 1.8mm and plus or minus 0.08mm on 2.0mm, so the bending team sets tooling once per gauge rather than per bundle. Flatness is controlled to within 3mm per metre after tension levelling, which keeps laser-cut cabinet blanks from rocking on the welding table. Every sheet is protected with a removable PVC film on the visible face, interleaved with paper, and edge-protected before packing, so the polished and hairline surfaces reach the workshop ready to fabricate. All shipments carry a mill test certificate listing heat number, chemical composition, mechanical properties and intergranular corrosion test results.
| Attribute | No.4 HL Finish | BA Finish |
|---|---|---|
| Surface appearance | Continuous hairline grain, satin brushed | Bright, mirror-like reflective |
| Production route | Abrasive belt polishing after annealing | Bright annealing in controlled atmosphere |
| Roughness (Ra) | 0.4 – 0.8 micron | 0.05 – 0.2 micron |
| Typical use | Cabinet fronts, worktops, hood panels | Splashbacks, liners, display cases |
| Fingerprint visibility | Low, grain masks marks | Higher, benefits from anti-fingerprint film |
| Repairability on site | Re-polishable along the grain | Difficult to spot-repair |
| Parameter | Specification |
|---|---|
| Grade | 304 (UNS S30400 / 1.4301) |
| Finish | No.4 HL (hairline) and BA (bright annealed) |
| Thickness | 1.5mm / 1.8mm / 2.0mm |
| Thickness tolerance | ±0.05mm (1.5 / 1.8mm), ±0.08mm (2.0mm) |
| Width | 1219mm / 1500mm |
| Length | 2438mm / 3000mm, cut to size on request |
| Flatness | ≤3mm per metre |
| Tensile strength | ≥515 MPa |
| Yield strength | ≥205 MPa |
| Elongation | ≥40% |
| Surface protection | PVC film on visible face, paper interleaved |
| Standard | ASTM A240, EN 10088-2 |
- Single-mill sourcing eliminated shade and grain mismatch, removing the re-polishing step from most cabinet runs.
- Tight gauge control let the bending team standardise tooling per thickness, cutting set-up time and springback scrap.
- Film and interleaved packing reduced transit surface damage to a negligible level on arrival inspection.
- Consolidated shipments shortened replenishment from six to eight weeks down to three to four weeks.
- Heat-number traceability and ASTM A240 certificates satisfied project specifiers and hotel group auditors.
- Both finishes now come from one supplier, simplifying purchase orders, claims and stock planning.
For a fabricator selling finished stainless steel kitchens, surface consistency matters as much as the alloy itself. By locking 304 No.4 HL and BA sheet in 1.5mm, 1.8mm and 2.0mm to one mill and one polishing line, the Malaysian buyer turned a chronic rework problem into a predictable process, and gained the documentation and delivery rhythm to bid larger hotel projects with confidence.

